Wedge Conveyor
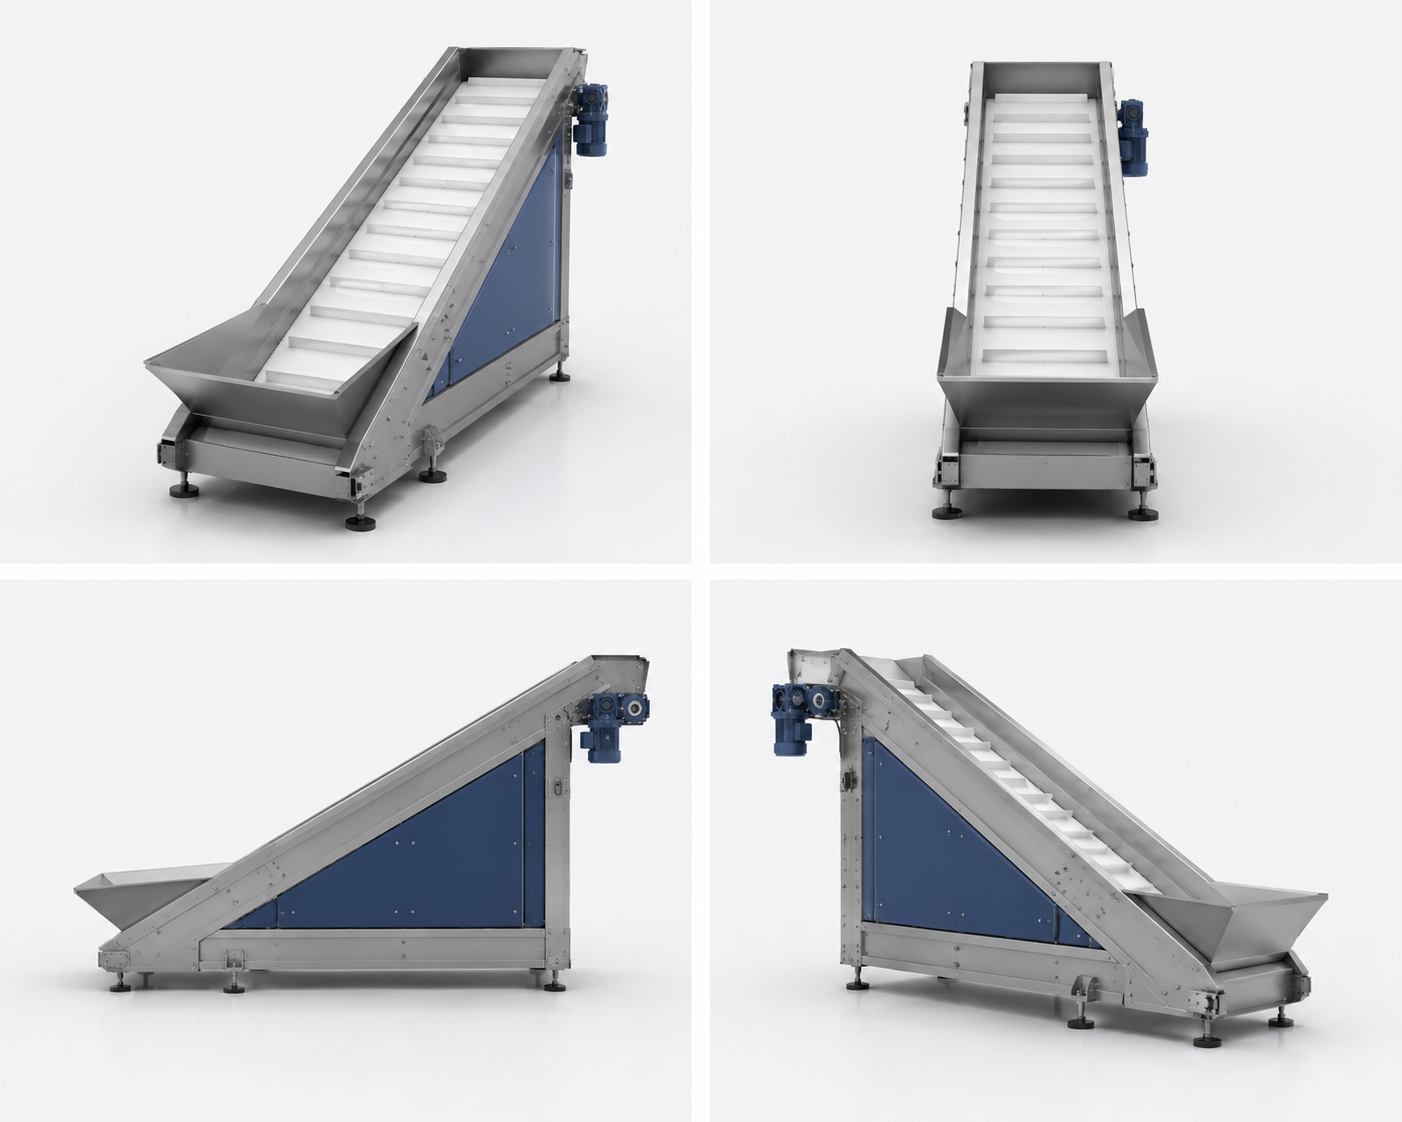
A Wedge Conveyor is a specialized conveyor system designed to transport products vertically or at steep inclines by securely gripping them between two synchronized side belts. This innovative conveying method enables manufacturers to maximize floor space, improve production flow, and automate product transfer between different levels without compromising product stability. Whether handling bottles, containers, cartons, pouches, or packaged goods, a wedge conveyor provides reliable and efficient vertical transportation.
At OSTECH, we design conveyor solutions that combine precision engineering, durability, and automation to meet the demands of modern manufacturing environments. As an experienced Wedge Conveyor Manufacturer, we develop customized conveyor solutions that integrate seamlessly with automated production lines while ensuring smooth and consistent product movement.
Our Wedge Conveyor System is built for continuous industrial operation and can be configured for different product sizes, production capacities, and factory layouts. From standalone applications to complete end-of-line automation, OSTECH helps manufacturers improve efficiency, reduce manual handling, and optimize available floor space.
Key Highlights
Secure side-grip product handling
Efficient vertical product transportation
Heavy-duty industrial construction
Smooth and continuous operation
Compact space-saving design
Easy integration with automated production lines
Low maintenance requirements
Suitable for multiple industries
What is a Wedge Conveyor?
A Wedge Conveyor is a conveyor system that transports products by holding them securely between two synchronized side belts. This design allows products to move vertically or along steep inclines while maintaining stability throughout the conveying process.
A modern Wedge Conveyor System is widely used where factory floor space is limited and products need to move between different production levels. Unlike conventional conveyors, a Wedge Belt Conveyor securely grips products from both sides, minimizing movement and reducing the risk of product damage during transportation.
Often referred to as a Side Grip Conveyor, this conveyor is ideal for handling bottles, jars, cartons, containers, cans, pouches, and similar products that require stable vertical movement. As an Automatic Wedge Conveyor, it integrates easily with filling machines, packaging equipment, labeling systems, and case packers to create a fully automated production line.
Key Features of the Wedge Conveyor
Every OSTECH wedge conveyor is engineered to provide reliable performance and long-term durability in demanding industrial environments.
Secure Side Grip Design
The Side Grip Conveyor securely holds products between two synchronized belts, ensuring stable movement even during vertical transportation.
Benefits include:
Improved product stability
Reduced product damage
Consistent product alignment
Smooth transportation
Vertical Product Transportation
Designed as a Vertical Wedge Conveyor, the system efficiently transfers products between different production levels while reducing floor space requirements.
Advantages include:
Maximum space utilization
Efficient vertical transfer
Continuous product movement
Optimized production layouts
Automatic Operation
As an Automatic Wedge Conveyor, the system automates product transfer between production processes while minimizing manual intervention.
Manufacturers benefit from:
Higher productivity
Continuous operation
Reduced labour dependency
Improved workflow
Heavy-Duty Industrial Construction
Every Industrial Wedge Conveyor is manufactured using durable industrial-grade materials designed to withstand continuous production and demanding operating conditions.
Key benefits:
Long operational life
Reliable industrial performance
Low maintenance
Stable product handling
Seamless Equipment Integration
The conveyor integrates efficiently with:
Filling machines
Packaging machines
Labeling systems
Case packers
Inspection equipment
Robotic systems
Palletizers
This integration helps manufacturers create efficient automated production lines.
Benefits of Using a Wedge Conveyor
A well-designed Wedge Conveyor System offers more than vertical transportation. It improves production efficiency, optimizes factory layouts, and supports long-term automation goals.
Increase Productivity
Continuous automated transportation keeps products moving efficiently between different production stages.
Business benefits include:
Higher production output
Faster manufacturing cycles
Reduced bottlenecks
Improved operational efficiency
Optimize Floor Space
A Vertical Wedge Conveyor allows manufacturers to utilize vertical space effectively, reducing the need for long horizontal conveyor systems and improving factory layout efficiency.
Improve Product Handling
The Wedge Belt Conveyor securely grips products throughout transportation, reducing product movement and minimizing handling damage.
Lower Operating Costs
Reliable automation reduces manual handling, improves equipment utilization, and lowers long-term operating costs.
Applications Across Industries
The Wedge Conveyor is widely used in industries where products need to be transported vertically while maintaining stability and continuous production flow. Its compact design makes it an ideal solution for manufacturers looking to optimize floor space and automate product transfer.
Food Processing
Food manufacturers use a Vertical Wedge Conveyor to transport bottles, jars, pouches, trays, and packaged food products between filling, labeling, packaging, and inspection stations while maintaining product alignment.
Beverage Industry
Beverage production lines rely on a Side Grip Conveyor to elevate PET bottles, glass bottles, cans, and containers without damaging the products or interrupting production.
FMCG Manufacturing
An Automatic Wedge Conveyor helps FMCG manufacturers move products efficiently between multiple production levels, improving throughput while reducing manual handling.
Pharmaceutical Industry
An Industrial Wedge Conveyor transports medicine bottles, cartons, blister packs, and healthcare products safely between manufacturing and packaging processes while ensuring smooth product flow.
Personal Care & Cosmetics
Manufacturers use wedge conveyors to handle shampoo bottles, lotion containers, cosmetic products, and personal care packaging with consistent positioning throughout automated production lines.
Chemical & Industrial Manufacturing
Industrial facilities use wedge conveyors for transporting containers, cans, and packaged products where reliable vertical conveying and space optimization are essential.
How the Wedge Conveyor Works
The Wedge Conveyor System uses two synchronized side belts to securely grip products and transport them vertically or along steep inclines without affecting product stability.
Step 1 – Product Feeding
Products enter the conveyor from upstream equipment or a standard conveyor line.
Step 2 – Side Grip Transportation
The Side Grip Conveyor gently holds products between two moving belts, ensuring secure handling throughout transportation.
Step 3 – Vertical Product Transfer
The Vertical Wedge Conveyor moves products upward or downward while maintaining consistent spacing and alignment.
Step 4 – Product Discharge
Products are released smoothly onto downstream equipment such as labeling machines, case packers, packaging systems, palletizers, or inspection stations.
Customization Options
Every production facility has unique automation requirements. OSTECH offers customized wedge conveyor solutions to ensure seamless integration with existing manufacturing systems.
Available Customizations
Conveyor height and length
Adjustable side belt spacing
Variable speed control
Stainless steel or mild steel construction
PLC and HMI integration
Sensor-based product detection
Product-specific gripping configuration
Safety guarding and emergency stop systems
Custom conveyor angles
Integration with complete production lines
These customization options allow manufacturers to maximize efficiency while supporting future production expansion.
Why Choose OSTECH?
Selecting the right conveyor partner is essential for achieving reliable production, efficient product handling, and long-term operational performance. OSTECH combines engineering expertise with practical industrial knowledge to deliver conveyor solutions that meet modern manufacturing requirements.
As a trusted Wedge Conveyor Manufacturer, we develop customized conveyor systems designed for reliable performance, smooth product handling, and easy automation integration.
We are also recognized as an experienced Industrial Wedge Conveyor Manufacturer, providing robust conveyor solutions that operate efficiently in demanding industrial environments.
Why Manufacturers Choose OSTECH
Customized conveyor solutions
Precision engineering
Heavy-duty industrial construction
Reliable long-term performance
Easy integration with automation systems
Experienced engineering team
Responsive after-sales support
Scalable solutions for future expansion
Customer-focused project execution
Whether you need a standalone Wedge Belt Conveyor or a complete Wedge Conveyor System, OSTECH provides reliable automation solutions tailored to your production requirements.
Explore Our Conveyor Solutions
Looking for a complete material handling solution? Explore our full range of Conveyor systems, including Belt Conveyors, Loading Conveyors, Slat Conveyors, Modular Conveyors, Retractable Conveyors, and Wedge Conveyors. Our comprehensive conveyor portfolio helps manufacturers build efficient, automated, and scalable production lines for a wide range of industries.
Related Products


Frequently Asked Questions
We provide conveyor systems, automatic case packers, wrap-around case packers, and custom material handling systems designed to increase production line efficiency.